Wear liners & chute plate
Quenched and tempered wear plate, chute and bin liners, skirting and deflector plate, cut and formed to your profile with hardness reports.
Crusher and mill spares, conveyor idlers and pulleys, chute and bin liners, screen components and structural fabrication. Manufactured to your drawing, inspected before dispatch and delivered to site at one landed price.
Quenched and tempered wear plate, chute and bin liners, skirting and deflector plate, cut and formed to your profile with hardness reports.
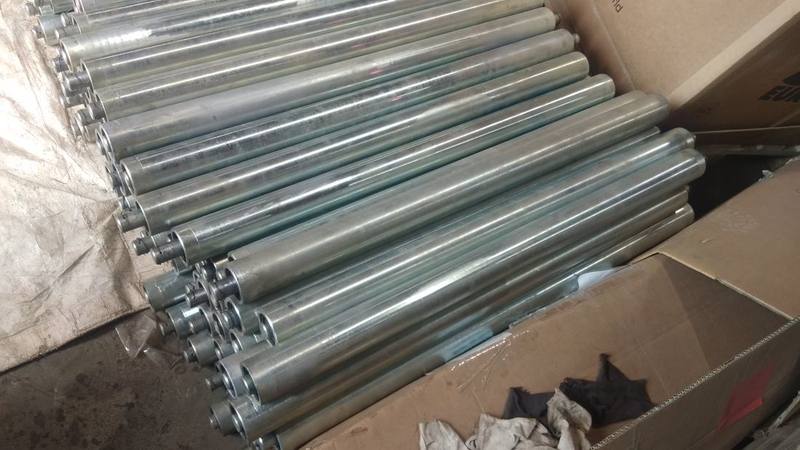
Idlers, rollers, pulleys, frames, brackets, drive components and take-up assemblies for fixed plant and mobile equipment.
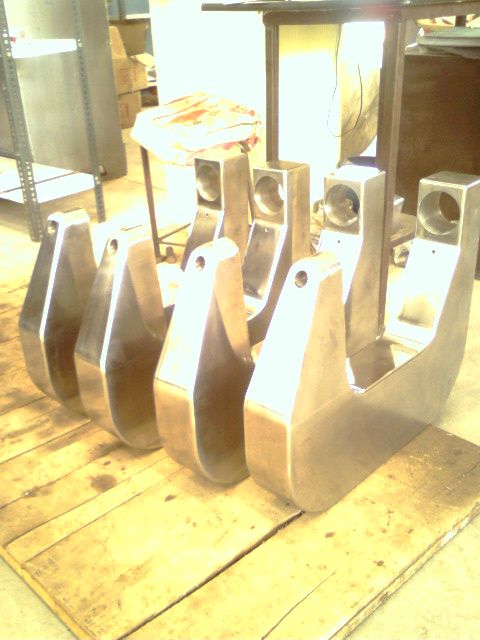
Machined and cast spares including bushes, housings, shafts, eccentric components and liner bolts, made to drawing and certified.
High tensile bolts, liner bolts, nuts, washers and coated hardware supplied in lot quantities with test certificates.
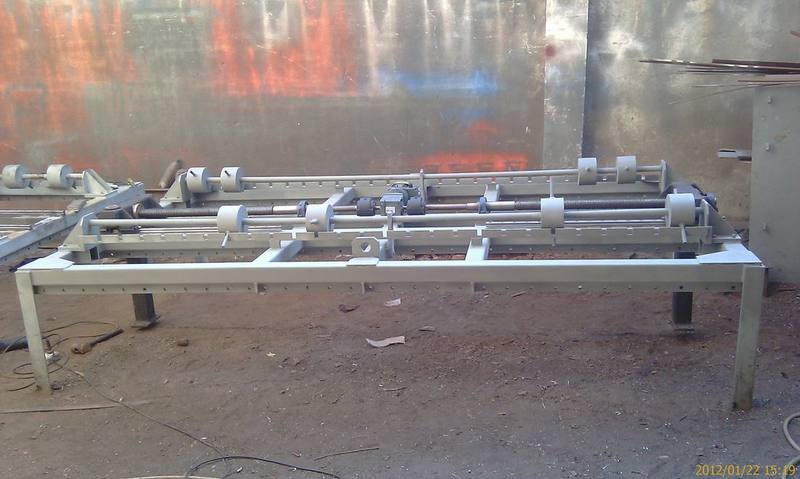
Walkways, platforms, support frames, hoppers and transfer chutes, fabricated to drawing and galvanised where required.
Moulded rubber lagging, skirting, sealing and polymer wear components for materials handling.
Most sites we speak to are not unhappy with their supplier. They are exposed to a single one. When a shutdown date is fixed and the only supplier quotes sixteen weeks, the cost of that exposure is measured in lost production, not in the price of the part.
That is the job we usually do first. We take a part you already buy, quote it against your current price and lead time, and hold the drawing so you can call it off later. If we cannot beat what you have, we will say so.
| Wear plate | 400 to 500 HB quenched and tempered, hardness tested and reported. |
|---|---|
| Castings | Grey iron, SG iron, cast and alloy steel, high chrome white iron for abrasion. Chemical and mechanical reports supplied. |
| Fabrication | Welded to a documented procedure, with weld inspection where the drawing calls for it. |
| Fasteners | Property class 8.8, 10.9 and 12.9 with mill certificates, coated or galvanised as specified. |
| Coating | Hot dip galvanising to AS/NZS 4680, or paint systems to your specification. |
Yes, where you own the drawing or the part is not covered by a current design right. Where you only have a worn sample we can often reverse engineer it, though we will tell you if the wear pattern makes the original geometry unclear.
Commonly 400 to 500 HB quenched and tempered plate, and higher chrome white irons where abrasion is severe. Tell us the ore, the impact condition and the current wear life and we will recommend rather than guess.
Typically eight to twelve weeks including sea freight where drawings exist and no tooling is needed. New casting patterns add four to six weeks. Air freight is available when a plant is down.
Yes, on repeat items with a forecast. We hold agreed quantities in Australia against your call-off so you draw from local stock rather than waiting on a container.
Inspection happens at the plant before dispatch, to an agreed plan, with dimensional and material reports. On a first order we cover the third-party inspection cost.